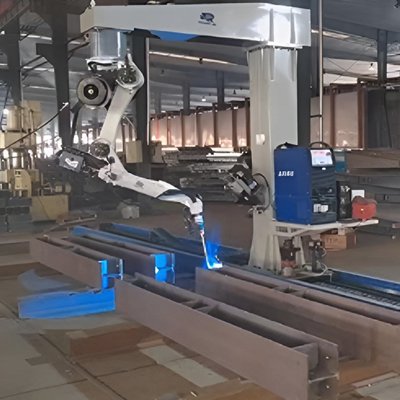
A Welding Robot is a programmable robotic arm fitted with a MIG, TIG, or plasma welding torch, built to run the same weld path repeatedly at a fixed speed and quality — the kind of repetitive weld work that's slow and inconsistent when done entirely by hand. ACM supplies welding robots to fabricators in Chhattisgarh and across North India who are automating repetitive weld jobs on components like brackets, frames, and structural sub-assemblies, without needing to replace their existing manual welding capacity entirely.
What is a Welding Robot? A Welding Robot is a multi-axis robotic arm fitted with a welding torch and controlled by a programmed path, used to perform MIG, TIG, or plasma welds with consistent speed, angle, and quality on repetitive jobs. It's typically taught a weld path once and then repeats it across identical parts.
How do I choose the right Welding Robot? Match the robot's reach and payload to your largest workpiece and torch weight, confirm the welding type (MIG/TIG/plasma) suits your material and joint type, and check whether your job mix is repetitive enough to justify automation over manual welding.
Welding Robot Supplier in Chhattisgarh
Manual welding on a repetitive job — the same bracket, the same frame joint, done fifty or a hundred times a shift — has a quality ceiling that's hard to push past. Even a skilled welder's angle, speed, and arc length drift slightly from piece to piece, especially past the second hour of a shift. A Welding Robot removes that drift: once a weld path is taught, it runs the same way every time, piece after piece.
That doesn't mean it replaces your welding floor. Most shops that bring in a welding robot keep manual welders for one-offs, prototypes, and awkward-geometry jobs, and route the repetitive, high-volume work to the robot instead. ACM supplies welding robots to fabricators around Chhattisgarh looking to make exactly that split — automate the repeatable work, keep manual capacity for everything else.
How Robotic Welding Actually Works
A welding robot is a multi-axis arm — usually 6-axis for full positional flexibility — with a welding torch mounted at the end. It doesn't "decide" how to weld; it follows a path an operator teaches it, either by manually guiding the torch through the weld once (teach pendant) or by programming coordinates directly. Once that path is set, the robot repeats it at a fixed speed, angle, and torch-to-work distance for every identical part fed to it.
The welding process itself — MIG, TIG, or plasma — is chosen based on material and joint type, same as manual welding. The robot doesn't change what welding process suits your material; it changes how consistently that process gets applied.
Choosing a Welding Type: MIG vs. TIG vs. Plasma
| Process | Best suited for | Speed | Finish quality |
|---|---|---|---|
| MIG (GMAW) | Mild steel, general fabrication, thicker sections | Fast | Good, some spatter |
| TIG (GTAW) | Thin sheet, stainless steel, precision joints | Slower | Very clean, minimal spatter |
| Plasma | High-precision cuts and welds on thinner material | Moderate-fast | Very precise, narrow heat-affected zone |
Most general fabrication shops running a welding robot for structural brackets and frames use MIG for its speed and tolerance for slight fit-up variation. TIG suits shops doing stainless or thin-gauge precision work where finish quality matters more than raw speed.
Applications
- General fabrication shops. Brackets, frames, and structural sub-assemblies with repetitive weld joints are the most common fit — high enough volume to justify programming time, consistent enough geometry to repeat reliably.
- PEB and structural steel component welding. Sub-assemblies and connection plates that feed into larger structural work benefit from consistent weld quality before final assembly.
- Automotive and heavy equipment component manufacturing. Repetitive joint welding on frames, chassis components, and equipment housings is a classic robotic-welding fit due to high part volume and repeatable geometry.
- Sheet metal and enclosure fabrication. TIG-capable robots suit thinner-gauge enclosures and panels where weld appearance matters as much as strength.
Specifications (Typical Range)
| Parameter | Typical Range |
|---|---|
| Axes | 6-axis |
| Reach | 1.4 m – 3 m |
| Payload capacity | 5 kg – 50 kg (torch + tooling) |
| Robot weight | ~400 – 450 kg |
| Position repeatability | ±0.02 mm – ±0.05 mm |
| Welding type | MIG / TIG / Plasma |
| Power supply | 230V / 400V–480V, three-phase |
| Automation grade | Automatic / Semi-automatic |
Why Bring In a Welding Robot
- Consistent weld quality across a full shift. The robot's speed, angle, and torch distance don't drift with fatigue the way a manual welder's can over a long run.
- Higher throughput on repetitive jobs. Once a path is taught, cycle time per part is predictable and generally faster than manual welding on the same joint.
- Frees skilled welders for harder work. Routing repetitive jobs to the robot lets your manual welders spend more time on one-offs, repairs, and complex geometry where their judgment actually matters.
- Reduced rework from inconsistent welds. Fewer weld-quality rejects at inspection when the same path and parameters are applied every time.
- Predictable production planning. Cycle time per part becomes a known number, which makes scheduling and quoting turnaround times more reliable.
Fixed-Arm Cell vs. Positioner-Integrated Setup
| Setup | What it means | Best for |
|---|---|---|
| Fixed-arm robotic cell | Robot arm welds a stationary or manually-loaded part | Simpler jobs, lower budget, smaller parts |
| Positioner-integrated setup | Robot works alongside a rotating/tilting positioner that presents the part at the right angle | Complex geometries, multi-sided welds, higher-volume production |
A positioner adds cost but removes the need to manually reposition parts mid-weld, which matters more as part complexity or volume goes up. For simpler, mostly-flat weld joints, a fixed-arm cell is usually the more cost-effective starting point.
Why Source It From ACM
ACM supplies welding robots to fabricators in Chhattisgarh and across North India, and can help match reach, payload, and welding type to the parts you're actually running rather than a generic listing spec.
If cost relative to manual welding capacity is the concern: talk through your actual part volume and repeat-job mix with ACM before comparing robot cost to welder wages directly — the payback calculation depends heavily on how repetitive your job mix really is, and it's worth checking that assumption before committing.