Every H-beam that comes off a welding line carries some amount of distortion — flange tilt, web camber, twist along the length. It's not a defect in the welding process; it's physics. Heat goes in unevenly during welding, the steel cools unevenly, and the beam comes out slightly bent in one plane or another. Left uncorrected, that distortion shows up later as misaligned bolt holes, uneven bearing surfaces, or a beam that simply won't sit flush during erection.
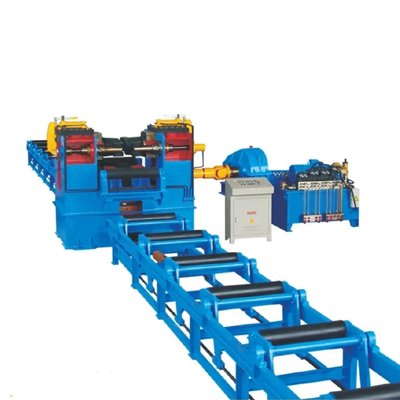
That's the job an H-Beam Straightening Machine does. It applies controlled, localized hydraulic pressure to push the flange and web back into tolerance — not by brute force, but by reading the deformation and correcting it in the specific plane it occurred.
In one line: an H-Beam Straightening Machine corrects flange tilt, web deviation, and camber in fabricated or rolled H-beams so they meet IS/structural tolerance before dispatch or erection.
ACM manufactures and supplies these machines from Hisar, built for PEB fabricators, structural steel plants, and beam-line operators who need this correction step to keep pace with their welding and cutting lines rather than becoming the bottleneck.
Myth vs. Reality: What Buyers Often Get Wrong
| The Assumption | The Reality |
|---|---|
| "Straightening is a manual, hammer-and-eye job" | A hydraulic H-Beam Straightening Machine applies measured, repeatable pressure — manual correction on large beams is slow and inconsistent by comparison |
| "One machine size fits all beam ranges" | Flange width, web height, and thickness capacity vary significantly between models — sizing to your actual beam range matters more than buying the biggest available machine |
| "Mechanical and hydraulic types are basically the same" | Mechanical units typically top out around 40mm flange thickness; hydraulic units go well beyond that — the two aren't interchangeable for heavier sections |
| "Straightening machines are only for PEB manufacturers" | Railway bridge fabrication, heavy structural steel, and general beam-line operations all use the same correction process |
Built For — Not Generic "Applications"
- PEB manufacturers running beam lines need straightening between welding and final dispatch — this is usually the last correction point before a beam ships to site.
- Structural steel fabricators cutting and welding custom sections see more variable distortion than standardized rolled beams, since every weld sequence introduces its own heat pattern.
- Railway bridge fabrication work often specifies tighter straightness tolerances than standard construction, making a dedicated hydraulic straightening step closer to mandatory than optional.
- Heavy equipment and machinery base frames — anywhere an H or I-section forms a load-bearing frame member, uncorrected camber becomes a downstream alignment problem.
Why ACM (Ansari CNC Machinary)
ACM manufactures and supplies H-Beam Straightening Machines from its Hisar facility, on the Grand Trunk Road corridor near Bahalgarh — which matters less as a location detail and more for what it means practically: shorter lead time for site visits, installation support, and spare parts than sourcing from an out-of-state or imported supplier.