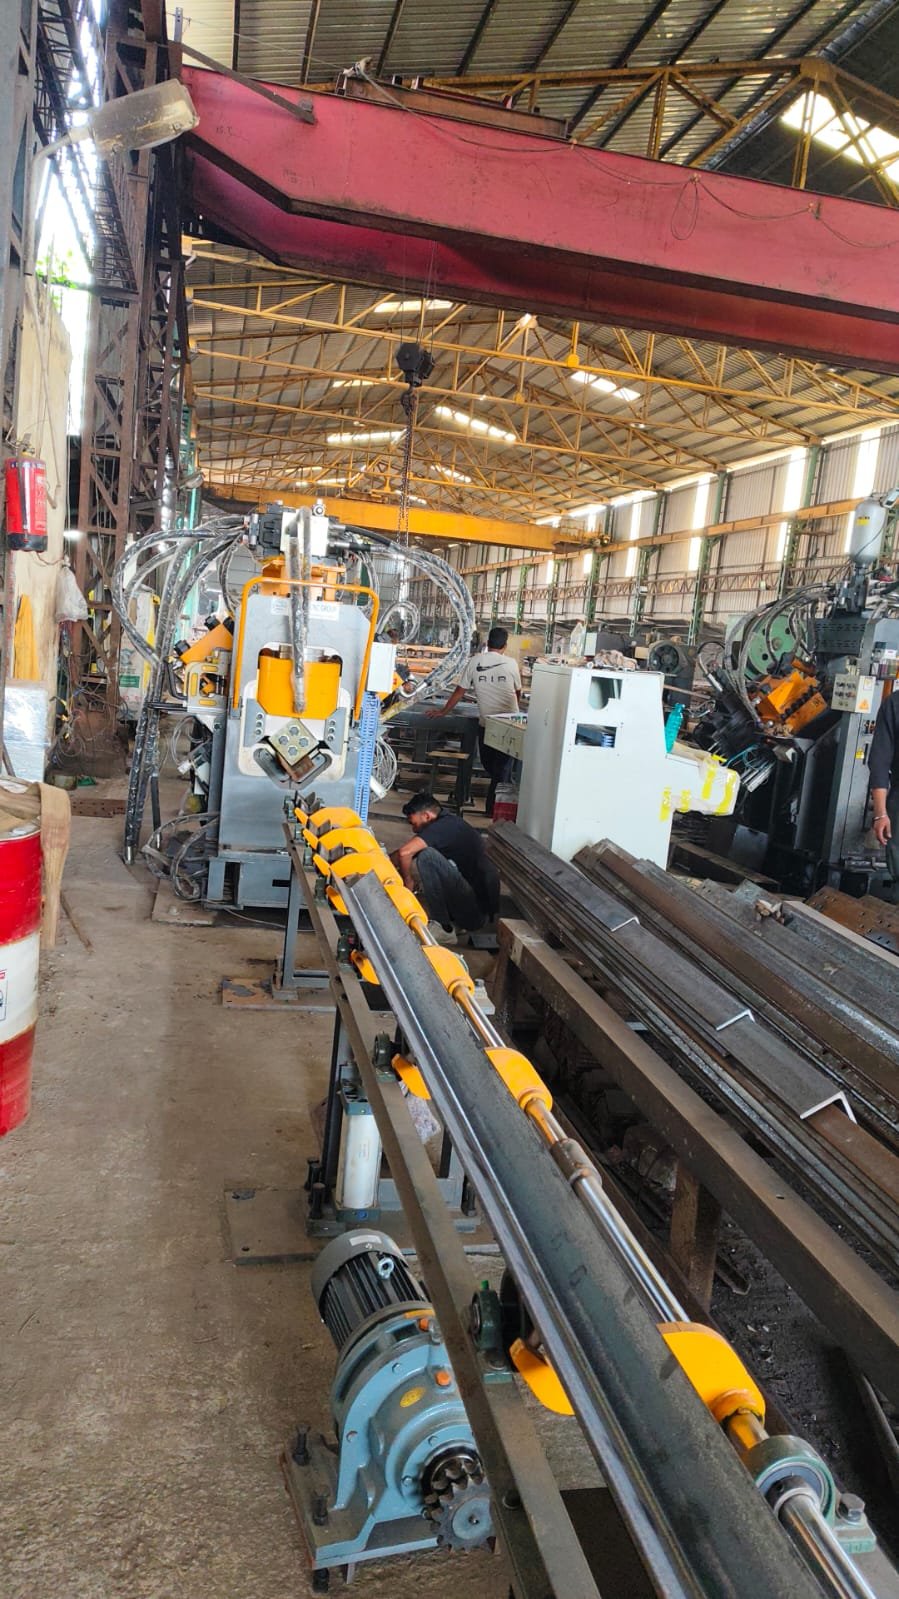
A CNC Angle Punching & Shearing Machine combines hole punching and length cutting into a single production line for structural steel angle sections — the angle is marked, punched with bolt holes at CNC-programmed positions, and sheared to length in one continuous pass, instead of moving between separate machines for each step. It's a core piece of equipment for telecom tower, transmission tower, and PEB structure fabricators who process large volumes of angle sections with repeat hole patterns. ACM supplies these machines to fabricators in Chhattisgarh and across North India working in tower and structural steel manufacturing.
What is a CNC Angle Punching & Shearing Machine? A CNC Angle Punching & Shearing Machine punches bolt holes into structural steel angle sections at CNC-programmed positions and shears the angle to length, combining both operations into one production line instead of requiring separate punching and shearing machines.
How do I choose the right CNC Angle Punching & Shearing Machine? Match the machine's angle size capacity and max thickness to the largest angle section you process, confirm punching tonnage suits your hole sizes and plate thickness combination, and check whether your volume justifies a combined punch-and-shear line over separate machines.
CNC Angle Punching & Shearing Machine Supplier in Chhattisgarh
Telecom towers, transmission towers, and PEB structures are all built from angle sections with dozens of repeat bolt-hole patterns — the same hole spacing, showing up on hundreds of identical angle pieces across a single tower or building order. Punching those holes by hand, or on a separate machine from the one that cuts the angle to length, means moving the same piece of steel between stations multiple times. A CNC Angle Punching & Shearing Machine does both in one line: mark, punch, and shear, without re-handling the angle in between.
That matters more than it sounds like on paper. Every extra handling step on a long angle section is a chance for it to shift out of position, which throws off hole alignment relative to the cut end. ACM supplies CNC angle punching and shearing machines to fabricators in Chhattisgarh and across North India producing angle sections for tower manufacturing, PEB structures, and solar mounting structures, where repeat accuracy across hundreds of identical pieces is the whole point.
How the Combined Line Works
The process runs in sequence on one machine: the angle stock feeds in, a CNC-controlled system marks and punches bolt holes at programmed positions along the angle's length, and once the punching pattern is complete, the shearing station cuts the angle to its final length. Because the piece doesn't leave the machine between punching and shearing, hole position stays fixed relative to the cut end — there's no re-clamping step where alignment could drift.
For repeat orders — the same angle size, same hole pattern, same length, produced across dozens or hundreds of pieces — this sequence gets programmed once and then repeats identically, piece after piece.
Specifications
| Parameter | Value |
|---|---|
| Angle size capacity | 150 x 150 mm |
| Overall capacity | 150 Ton |
| Punching capacity | 120 Ton |
| Max thickness | 16 mm |
| Punch shape | Round |
| Operation | Hydraulic |
| Automation grade | Automatic |
| Voltage | 415 V |
| Power source | Hydraulic |
| Delivery time | 40–45 days |
Why Combine Punching and Shearing Instead of Using Separate Machines
- Fewer handling steps mean fewer alignment errors. Every time an angle section is unclamped and moved to a different machine, there's a chance of repositioning error. A combined line eliminates that step between punching and shearing.
- Faster cycle time on repeat-pattern jobs. Once a hole pattern and length are programmed, the machine repeats the full sequence without an operator manually transferring pieces between stations.
- Less floor space and material handling infrastructure needed compared to running separate dedicated punching and shearing machines side by side.
- Better fit for high-volume, repeat-geometry work — tower legs, bracing members, and PEB angle framing typically involve exactly this kind of repeat pattern across large quantities.
Applications
- Telecom and transmission tower manufacturing. Tower legs and bracing members are almost entirely angle sections with repeat bolt-hole patterns — this is the primary use case for this machine type.
- PEB (Pre-Engineered Building) structure fabrication. Angle bracing and secondary framing members in PEB structures often need the same punch-and-shear treatment as tower components.
- Solar mounting structure manufacturing. Ground-mount and rooftop solar structures use large volumes of punched angle sections for racking and support frames.
- Power transmission line and electrical tower components. High-tension line towers and substation structures rely on precisely punched angle sections at scale.
Why Source It From ACM
ACM supplies CNC angle punching and shearing machines to fabricators across Chhattisgarh and North India, and can help match angle size capacity, punching tonnage, and thickness rating to the profiles you're actually processing.
If price relative to running separate punching and shearing machines is a concern: work out your actual repeat-pattern volume with ACM before deciding — the combined line's advantage grows with volume and repeat geometry, so it's worth checking that assumption against your real order mix.